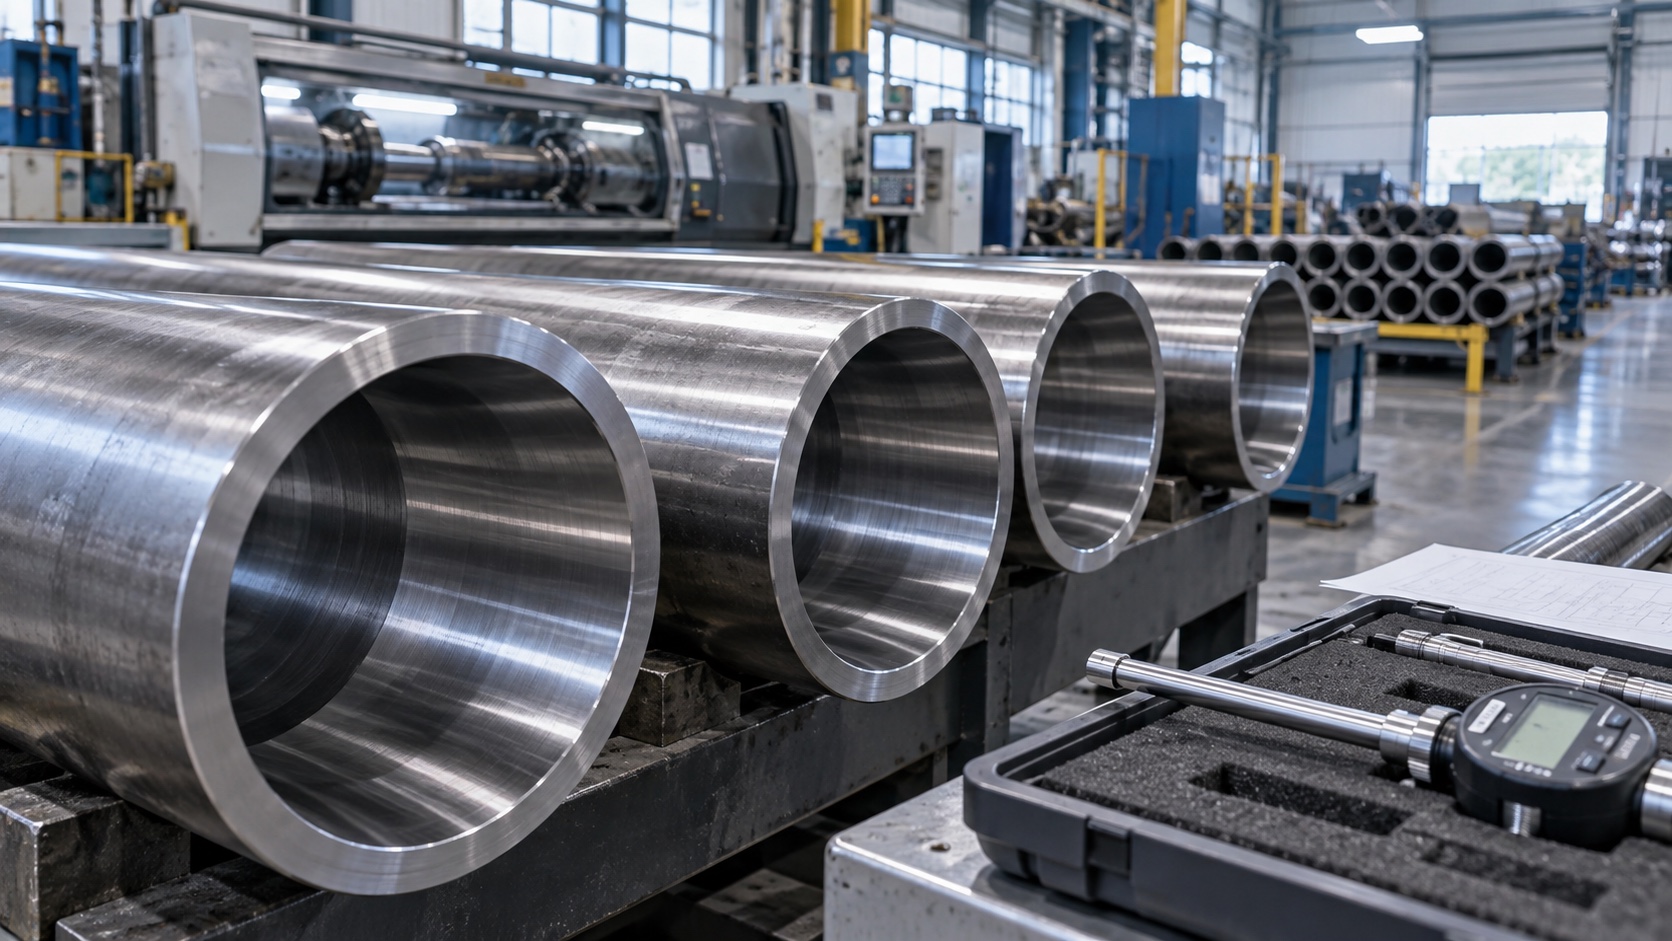
A hydraulic cylinder honed tube is a precision-finished cylinder barrel whose inside diameter, geometry and surface texture are controlled for reliable piston-seal movement. Buyers should specify much more than nominal OD and wall thickness: the purchase order should identify the governing standard, steel grade, delivery condition, finished bore size and tolerance, surface parameters, straightness, length, testing and preservation.
For a project-specific quotation, review New Star Steel’s Hydraulic Cylinder Tube range and provide the cylinder drawing, annual quantity and required inspection level.
Ordinary mechanical tubing can be suitable as a machining blank, but a ready-to-use cylinder barrel has a functional bore. The piston seal runs directly against that surface. Bore diameter, roundness, cylindricity, straightness and texture therefore affect friction, leakage, seal wear and service consistency.
Honing is a controlled abrasive finishing process used after boring, drawing or other preparation. Sunnen’s technical guidance describes honing as a final operation for improving bore geometry and surface finish. The finished surface normally retains a cross-hatch that supports lubrication, but the correct texture must be agreed with the seal supplier rather than selected from a generic catalog value.
| RFQ item | What to state | Why it matters |
|---|---|---|
| Standard and grade | For example, EN 10305 delivery requirements and E355, or ASTM A519 with a specified SAE grade | Controls chemistry, mechanical properties, inspection and documentation |
| Finished bore | Nominal ID, tolerance class or numerical limits, and allowance before/after any local machining | Determines piston and seal fit |
| Surface texture | Required Ra/Rz or a seal-maker-approved texture specification | Influences friction, oil retention and seal life |
| Geometry | Straightness, ovality, wall eccentricity and end squareness | Prevents assembly and machining problems |
| Length and ends | Fixed/random length, cutting tolerance, chamfering and deburring | Reduces downstream processing |
| Inspection | 3.1 certificate if required, dimensional report, roughness record and NDT requirements | Creates traceable acceptance evidence |
Start with the design load, weldability, machining route and regional standard. E355 is commonly specified in the EN precision-tube system; SAE 1026 is a chemistry-based carbon-steel designation used with North American specifications. ST52 remains common in legacy drawings and commercial language, but it should not be treated as an automatic one-to-one substitute for E355 without checking the applicable edition, delivery condition and required properties.
Our detailed E355 vs ST52 vs SAE 1026 honed tube guide explains how to compare these requests without relying on a grade-name shortcut.
Both processes can create a seal-ready cylinder bore. Honing removes material with bonded abrasive stones and is highly adaptable when geometry correction and a controlled cross-hatch are important. Skiving and roller burnishing (SRB) combines cutting to size with plastic smoothing of the surface; it is widely chosen for high-throughput tube production.
The right decision depends on bore range, length, starting-stock variation, production volume and the exact surface required by the sealing system. See the practical comparison in Honed Tube vs SRB Tube.
A low Ra value alone does not fully describe a functional bore. Peak shape, valley structure, material ratio and waviness can change sealing behavior even when two parts have the same arithmetic roughness. SKF’s hydraulic sealing guidance gives process-dependent recommendations for honed or roller-burnished cylinder bores and demonstrates why buyers should align tube requirements with seal material and pressure duty.
Ask the supplier how roughness is measured, where readings are taken and whether the report covers the full production lot or only a first-piece sample.
The most frequent errors are ordering only by trade name, accepting an “equivalent” grade without an agreed comparison, confusing tube OD tolerance with finished bore tolerance, and leaving preservation undefined. Another mistake is quoting a very low roughness value while ignoring seal-maker recommendations or the need for lubricant-retaining valleys.
A good RFQ includes a drawing and separates mandatory acceptance criteria from preferred targets. This gives the mill a clear basis for process selection and gives the buyer objective inspection points.
It can be, provided the delivered bore, geometry, surface texture, material condition and cleanliness match the cylinder design. Ports, threads, end machining and welding may still be required.
Use the tolerance required by the piston, guide and seal design. A familiar tolerance class is not a substitute for checking the entire fit and the supplier’s achievable process capability.
Many carbon-steel grades are weldable, but the welding procedure, carbon equivalent, heat-affected-zone properties, cleanliness and post-weld distortion must be evaluated for the actual grade and delivery condition.
Need a production quotation? Send the drawing, grade, finished bore, tolerance, surface requirement, length, quantity and certificate requirement through New Star Steel’s contact page.