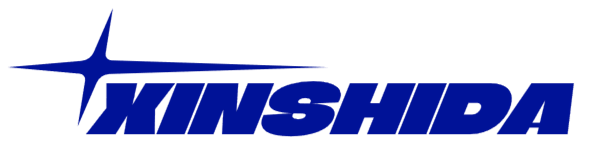
Honed tube and SRB tube can both provide a precision bore for hydraulic cylinders, but they create that bore in different ways. Honing is an abrasive cutting process that can correct bore geometry and generate a cross-hatched texture. Skiving and roller burnishing (SRB) cuts the bore to size and then plastically smooths the peaks, making it especially attractive for repeatable, high-volume production.
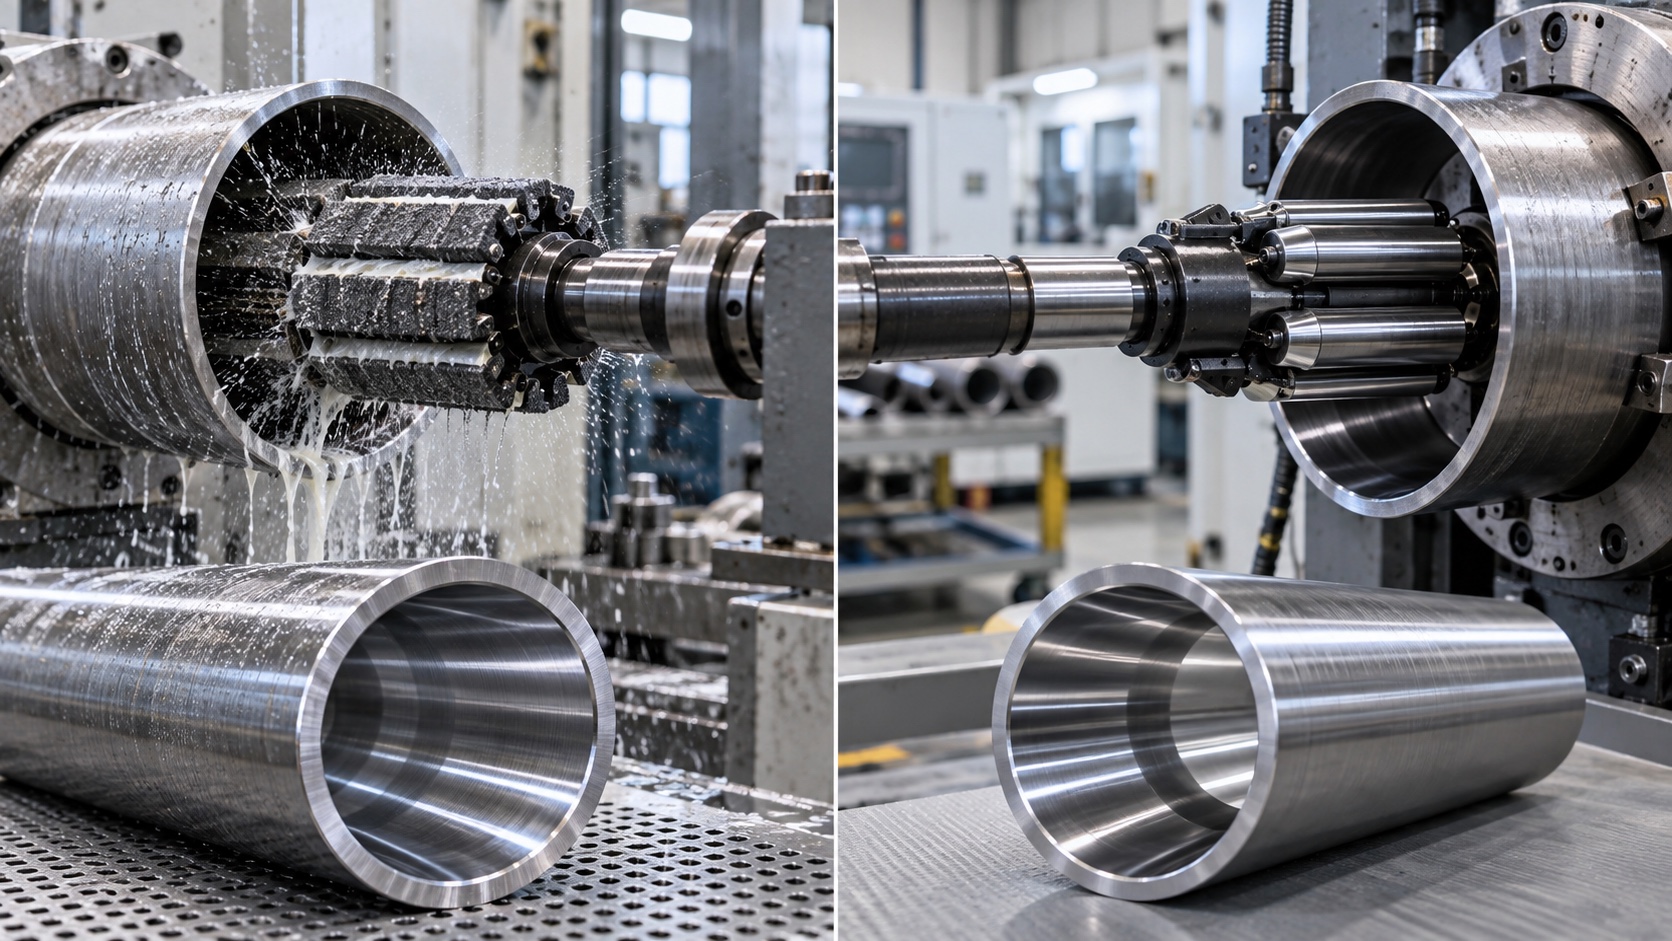
The best specification is not “the smoothest process.” It is the process that reliably delivers the diameter, form and functional surface required by the seal system at the project’s volume and cost. New Star Steel supplies hydraulic cylinder tube in process routes matched to the drawing and application.
During honing, abrasive stones contact the bore while the tool rotates and reciprocates. The controlled overlap helps improve size, roundness, straightness and surface texture. Honing can be applied to new tubes and to bores that need corrective finishing.
SRB combines two operations. Skiving removes a controlled layer to establish bore size and geometry. Roller burnishing then presses the surface peaks, producing a smoother, work-hardened near-surface layer without a second abrasive operation. ECOROLL’s process description explains this cutting-and-forming sequence.
| Decision factor | Honed tube | SRB tube |
|---|---|---|
| Finishing principle | Abrasive material removal | Skiving followed by plastic smoothing |
| Typical visual texture | Controlled cross-hatch | Very smooth, plateau-like burnished surface |
| Geometry correction | Flexible for correcting bore form | Strong repeatability when starting stock and setup are controlled |
| Productivity | Usually lower material-removal rate | Often faster for long production runs |
| Surface modification | Cuts the surface | Burnishing can raise bearing area and strain-harden the surface layer |
| Best choice | Complex correction, service work, controlled cross-hatch | High-volume new production and efficient one-pass finishing |
Arithmetic roughness is useful, but it compresses a complex surface into one number. Two bores can share the same Ra while having different peak sharpness, valley depth, waviness and material ratio. Those differences can change break-in behavior, lubricant retention and seal wear.
SKF’s hydraulic seal guidance treats honed and roller-burnished bores as functional counter-surfaces and recommends evaluating several roughness parameters. The practical lesson is simple: obtain the seal supplier’s counter-surface specification, then require the tube producer to report the relevant measurements.
ECOROLL reports that combined skiving and burnishing can achieve dimensionally accurate bores with low roughness in one process chain. Those published tool capabilities are useful engineering references, but a purchase order should still state acceptance limits rather than relying on a process name.
Specify material grade and standard, delivery condition, nominal finished ID with upper and lower limits, OD and wall requirements, roundness or cylindricity where necessary, straightness, surface parameters, length, end condition, cleanliness and corrosion protection. Add sample frequency and report format for dimensional and roughness inspection.
If the drawing says only “honed” or “SRB,” suppliers may quote different acceptance levels. A complete functional specification gives you comparable offers.
Not necessarily. Both processes cover a range of finishes. The result depends on tooling, stock allowance, material, machine stability and the measurement method.
No. It is a highly productive option, but blind bores, repair work, unusual geometry, starting-stock variation or a specified cross-hatch may favor honing.
Seal life depends on the complete tribological system: surface texture, hardness, alignment, pressure, speed, lubrication, contamination and seal material. Process name alone cannot guarantee life.
For material selection, continue with E355 vs ST52 vs SAE 1026. For a drawing review and quotation, contact New Star Steel.